
- WEBSITE -

Current location: Home > BLOGS > Industry Information >
C and Z Purlin Roll Forming Machine: Selection and Application Guide
Time:2026-10-12 02:42:40 Author:xiangyi Click:107
C and Z Purlin Roll Forming Machine: Selection and Application Guide
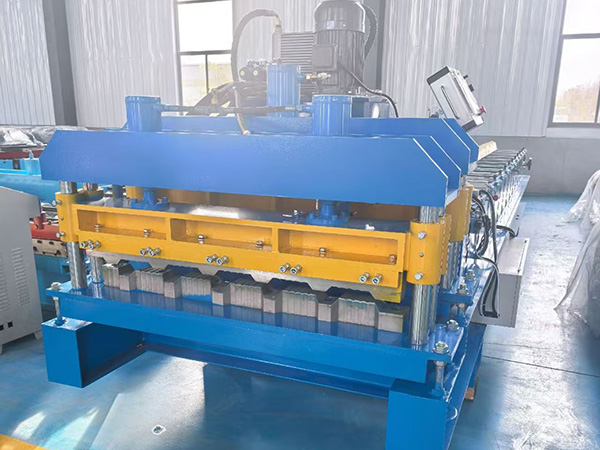
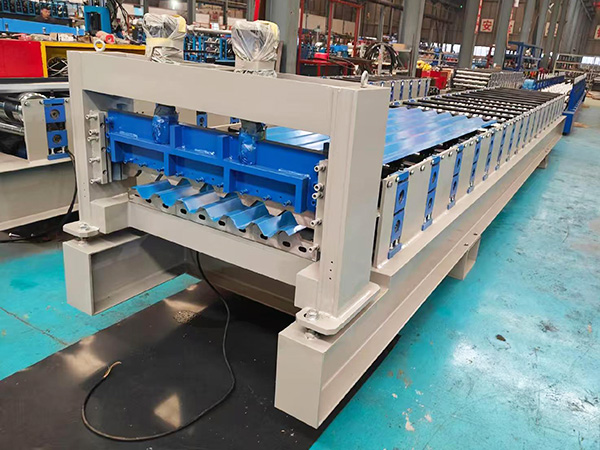
Purlins hold up the roof and walls of almost every steel building, and they are produced by the million on roll forming lines. A C and Z purlin roll forming machine is the equipment behind that output, turning galvanised coil into the structural sections that carry cladding loads from the roof to the frame.
Choosing the right machine comes down to size range, changeover speed and how well the line matches the buildings you actually supply.
What Purlins Are and Where They Are Used
A purlin is a horizontal secondary member that spans between the primary frame of a building. C-section purlins have a channel shape with flanges; Z-section purlins are similar but with opposite flanges, allowing them to overlap and continue over supports. Both are common in warehouses, workshops, agricultural buildings and light industrial sheds.
Because roof spans vary, a single project needs several purlin sizes. That is why changeover flexibility matters as much as raw speed.
One Machine, Both C and Z Profiles
The practical advantage of a combined C and Z machine is that it forms both section types on one frame. Typically the line uses a common set of rolls with interchangeable or repositionable tooling, so the same machine can switch between a C profile and a Z profile without a second line.
This single-machine dual-use design suits factories that supply both roof and wall systems from one workshop. It reduces floor space and capital cost compared with buying two dedicated machines, at the price of some changeover time between profiles.


Size Range and Thickness
Purlin lines are usually specified by the height range they can form, for example 80 to 300 mm section depth, together with the material thickness range, commonly around 1.5 mm to 3.0 mm for structural purlins. Some lighter architectural purlin lines run thinner material.
Confirm the height range carefully. A machine that stops at 250 mm cannot be stretched to 300 mm later without new tooling, and shell projects often need the larger sizes.
Rapid Changeover and Automatic Adjustment
The main productivity factor on a purlin line is how long it takes to change size. Manual adjustment means moving spacer plates and resetting rolls by hand, which can take a long time on a multi-size order.
Automatic or semi-automatic changeover uses hydraulic or motorised adjustment to reposition the forming stations to a new size. On a line producing many purlin sizes in a day, automatic changeover is often the difference between keeping up with orders and losing them.
Punching, Cutting and Holes
Purlins usually need holes for bolting and slots for adjustment. Inline punching saves a separate operation and keeps hole positions accurate relative to the section. The cutting unit then slices the section to the ordered length.
Ask how the punching is configured, whether the dies are quick to change, and whether the line can run different hole patterns without stopping production for long. On structural work, hole accuracy is not cosmetic, it decides how quickly the building goes together on site.
Material and Coating
Purlin coil is normally hot-dip galvanised steel in the structural thickness range. The metallic coating resists corrosion, and the forming process must not crack it at the bend radii, particularly at the corners of the section.
Thicker structural steel is harder to form, and springback increases. A well-designed flower pattern compensates for this with enough forming stations and correct roll geometry, so the finished section meets the drawing rather than springing open at the flanges.
Matching the Line to Your Projects
List the sizes you actually quote. If most of your work sits in a narrow size band with occasional large sections, a mid-range machine with manual changeover may be enough. If you quote a wide spread of sizes every week, automatic changeover and a generous height range will earn their cost back quickly.
Consider throughput as well. A purlin line feeding a busy steel building market needs to run consistently, which favours a robust frame, reliable hydraulics and a control system that a trained operator can manage without constant specialist help.
Questions for a Purlin Machine Supplier
Ask for the exact height and thickness range, the changeover method and time, the punching configuration, and the control system features. Ask how the roll design handles the thicker end of your material range.
A manufacturer that answers these with specific figures is working from a real engineering basis. That matters on purlin machines more than almost anywhere else in roll forming, because the sections are structural and the tolerances carry load.
References
Roll Forming Handbook, edited by George T. Halmos, CRC Press, 2005.
Cold-Formed Steel Design, Wei-Wen Yu and Roger A. LaBoube, Wiley.
EN 1090-2:2018, Execution of steel structures and aluminium structures, Part 2: Technical requirements for steel structures.
EN 10162:2003, Cold-rolled steel sections, Technical delivery conditions, Dimensional and cross-sectional tolerances.
EN 10346:2015, Continuously hot-dip coated steel flat products for cold forming, Technical delivery conditions.
ASM Handbook, Volume 14B: Metalworking: Sheet Forming, ASM International, 2006.
S. Tehrani, J. Hartley, H. Moslemi Naeini and M. Khademizadeh, "Localized edge buckling in cold roll-forming of symmetric channel section," Thin-Walled Structures, Vol. 44, 2006.
CONTACTS
TEL:+8615830824095
URL:www.qiluomachinery.com
ADD:Botou City, Cangzhou City, Hebei Province